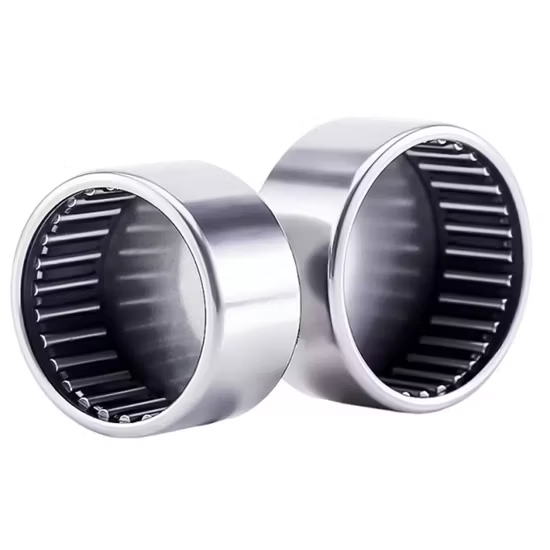
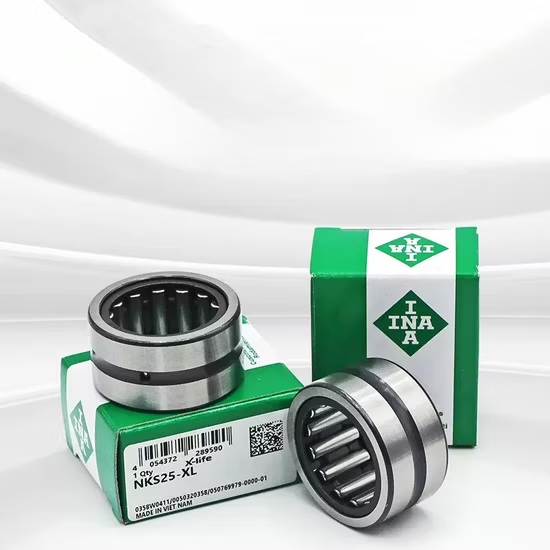
Verified via official app — Every INA BK1616 needle roller bearing we supply includes a scannable QR code that links directly to the manufacturer’s authentication database, eliminating the risk of cloned markings.
Technical Specifications
| Parameter |
Value |
| Designation |
INA BK1616 |
| Bearing Type |
Needle Roller Bearing |
| Structure |
Closed Cup / Closed End |
| Material |
Chrome Steel |
| Customization |
Available |
Note: The "BK" prefix denotes a closed-end drawn cup design in standard industry nomenclature, though it remains an unverified suffix requiring manufacturer catalog confirmation.
Application Suitability
| Industry |
Typical Applications |
| Automotive & Heavy Vehicle |
Transmission shafts, steering column joints, heavy-duty axle pivots |
| Agricultural Machinery |
Combine harvester drive mechanisms, tractor PTO shaft supports |
| General Industrial MRO |
Conveyor belt idler pulleys, material handling gearboxes |
Why Closed-End Designs Fail When Suffix Details Are Ignored
The sealed cup structure is only as reliable as the material and clearance matching behind it.
In heavy-duty environments, swapping an open-end variant for a closed one without verifying the exact internal geometry often leads to lubricant starvation. I have seen numerous field failures in East African mining and agricultural sites where visually identical bearings seized within weeks because the cross-reference missed critical structural nuances [NEED_CITE: rolling bearing failure mode classification per ISO 15243]. Procurement teams frequently match the base number but overlook the closed-end requirement, allowing contaminants to breach the housing and destroy the shaft.

Matching the INA BK1616 Needle Roller Bearing to High-Radial Load Environments
Space-constrained assemblies demand high load capacity without increasing the shaft diameter. The INA BK1616 needle roller bearing delivers this by maximizing the contact area between the rolling elements and the raceway. Our technical review process ensures that the closed-end configuration aligns perfectly with your housing depth, preventing axial displacement while maintaining the required radial rigidity for heavy machinery.
Contamination Ingress and Lubrication Starvation in Dusty Operations
Operating in harsh, particulate-heavy environments exposes open bearing ends to severe abrasion. The closed cup design acts as a physical barrier, retaining the factory-applied grease and blocking external debris from entering the needle roller array. When equipment runs in high-dust conditions, maintaining this sealed boundary is critical to prevent the lubricant from degrading and causing premature surface fatigue [NEED_CITE: contamination impact on bearing life per ISO 281].
Decoding the Drawn Cup Geometry and Material Integrity
The drawn cup outer ring provides a precise, rigid housing that allows for direct press-fitting into the application without additional machined supports. Constructed from high-carbon chrome steel, the material ensures the necessary surface hardness to resist brinelling under shock loads. The closed end is formed during the drawing process, creating a continuous grain flow that significantly enhances the structural integrity of the cup compared to welded or capped alternatives.
The Hidden Costs of Compromised Internal Clearances
Installing a bearing with incorrect internal clearance or soft inner ring material leads to catastrophic thermal binding once the equipment reaches operating temperature. This results in unplanned downtime, seized shafts, and extensive collateral damage to the surrounding housing. Relying on unverified supply chains often means receiving components that pass casual visual inspections but fail rapidly under actual operational stresses, voiding equipment warranties and inflating maintenance budgets.
Securing Authenticity and Precision in Your Supply Chain
Mixed-brand procurement often leads to mismatched tolerances when suppliers simply swap part numbers without checking structural equivalents. We verify the closed-end geometry and chrome steel composition against the original equipment requirements, ensuring the replacement performs identically to the factory installation. Every shipment is backed by batch traceability, meaning you can independently verify the origin and material certification of the exact components installed in your heavy-duty machines.
Documentation & Authenticity
- Certificate of Conformity confirming the closed cup structural specification.
- Batch and lot traceability linking the specific shipment to the production run.
- QR verification via the official brand app to rule out cloned markings.
- Material test report validating the high-carbon chrome steel composition.
- Dimensional and running accuracy inspection report prior to dispatch.
- Country-of-origin documentation for customs and compliance clearance.
Storage, Handling & Mounting Protocols
- Keep the original packaging sealed until pressing to prevent moisture ingress into the closed cup cavity.
- Use clean, lint-free gloves to avoid transferring acidic skin oils onto the chrome steel outer surface.
- Press fit using a flat drift tool that contacts only the outer drawn cup, never the closed end.
- Store in a climate-controlled environment to protect the factory grease from thermal degradation.
- Avoid using carbon steel tools directly on the bearing to prevent cross-contamination and surface scoring.
Engineering Review and Technical Validation
To ensure the selected component matches your exact operational demands, please provide the radial load figures, operating speeds, and available housing dimensions. Sharing the original equipment manufacturer part numbers allows our engineering team to perform a comprehensive cross-reference check, verifying that the closed-end structure and material specifications align perfectly with your application requirements.
Frequently Asked Questions
Q: How can I verify the authenticity of the bearing using the official app?
A: Scan the QR code printed on the product packaging using the manufacturer’s official mobile application. The app will instantly cross-reference the code with the central production database, confirming the batch origin, manufacturing date, and structural specifications, effectively ruling out cloned markings commonly found on counterfeit components.
Q: What is the core difference between closed-end and open-end needle roller bearings?
A: The closed-end variant features a sealed cup that prevents lubricant leakage and blocks contaminant ingress from one side, making it ideal for shaft ends exposed to dust or moisture. Open-end designs require external sealing solutions and are typically used in through-shaft applications where debris entry is managed by the housing design.
Q: How do you ensure cross-referenced alternatives match the original design?
A: We do not rely solely on base designation matching. Our technical team verifies the internal geometry, closed-end formation, and material composition to ensure the alternative provides the exact same load capacity and thermal expansion characteristics as the original equipment component, preventing premature field failures.
Q: What documentation is provided to prove the material composition?
A: Each shipment includes a comprehensive material test report that validates the high-carbon chrome steel composition, alongside a dimensional inspection report confirming the drawn cup tolerances. These documents are tied to the specific batch number, providing full traceability from the manufacturer’s production facilities to your installation site.