
22308-22312ek Self-Aligning Roller Bearing NSK NTN
View Details
SKF
-- SKF Authorized Engineering Partner
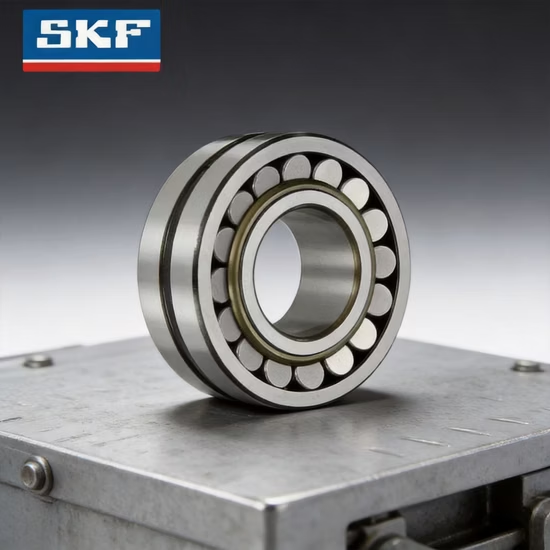
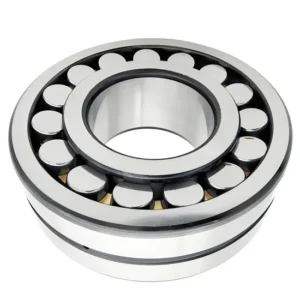
21312EK Spherical Roller Bearing 60×130×31 mm — engineered with a reinforced internal design for increased load capacity and a 1:12 tapered bore for precise clearance adjustment via adapter sleeves.
15+ Certified Engineers On-Call
Free application analysis · Failure diagnosis · Custom modification guidance. Response within 24 hours.
Cross-Reference Alignment Verified — Every 21312EK spherical roller bearing we supply strictly matches the base designation, the E reinforced internal geometry, and the K 1:12 tapered bore without exception.
| Parameter | Value |
|---|---|
| Designation | 21312EK |
| Bearing Type | Spherical Roller Bearing |
| Bore Diameter (d) | 60 mm |
| Outside Diameter (D) | 130 mm |
| Width (B) | 31 mm |
| Bore Type | Tapered 1:12 (K suffix) |
| Internal Design | Enhanced (E suffix) |
| Industry | Typical Applications |
|---|---|
| Mining and Crushing | Vibrating screen exciter mechanisms, jaw crusher pitman shafts |
| Steel and Metallurgy | Continuous caster roll segments, rolling mill gear drives |
| Industrial Gearboxes | Heavy-duty reduction gear output shafts, extruder drive housings |
| Pulp and Paper | Paper machine dryer cylinder journals, press roll bearings |
Ignoring the E and K suffixes during procurement turns a high-capacity component into a premature failure point.
I have seen countless shutdowns in heavy machinery because purchasing teams only verified the base 21312 number while overlooking the internal design and bore configuration. When a standard cylindrical bore variant is forced onto a tapered shaft, or when a non-reinforced internal design is subjected to severe vibrating screen loads, the equipment suffers rapid cage fatigue and thermal binding. Sourcing the exact 21312EK spherical roller bearing requires validating the reinforced roller profile and the precise taper angle to ensure the assembly survives the harsh realities of the plant floor [NEED_CITE: rolling bearing failure mode classification per ISO 15243].
Heavy industrial machinery demands components that can absorb massive shock loads while compensating for structural deflection. The 21312EK spherical roller bearing is engineered specifically for these punishing environments, where shaft misalignment is a constant threat rather than an occasional anomaly. By supplying this exact designation with verified cross-brand interchangeability, we ensure your maintenance team receives a component that drops directly into the existing housing without requiring makeshift adapters or compromising the original equipment manufacturer’s load calculations.
Vibrating screens and rock crushers generate severe multidirectional shock loads that quickly destroy inadequately specified components. The operating temperature in these enclosures often rises significantly, demanding a bearing internal clearance that accommodates thermal expansion without seizing the rolling elements. Proper lubrication flow is equally critical to flush out abrasive particulate matter that inevitably bypasses primary seals. Installing a component with the correct internal geometry ensures the load is distributed evenly across the roller profile, preventing localized stress concentrations that lead to spalling [NEED_CITE: bearing life calculation methods per ISO 281].
The E suffix denotes an enhanced internal design featuring a reinforced roller profile and optimized cage guidance, which substantially increases the dynamic load rating compared to standard base models. This structural upgrade is non-negotiable for applications involving heavy radial forces and continuous vibration. The K suffix specifies a 1:12 tapered bore, allowing the bearing to be mounted securely on a tapered shaft or via an adapter sleeve. This taper configuration enables maintenance crews to precisely adjust the radial internal clearance during installation by controlling the drive-up distance, ensuring the bearing operates with the exact preload required for the specific thermal and mechanical conditions of the application.
Substituting a standard bore or non-reinforced variant to save on initial procurement costs inevitably triggers unplanned downtime and catastrophic damage to adjacent shaft components. When the internal clearance is not correctly established via the tapered interface, the bearing either runs too loose, causing destructive skidding, or too tight, generating excessive friction heat. These installation errors void manufacturer warranties and force emergency shutdowns that halt entire production lines. Relying on verified documentation prevents these costly oversights and ensures the assembly meets the rigorous demands of continuous industrial operation.
Procuring mixed-brand requirements from a single authorized source eliminates the coordination delays and documentation gaps that plague multi-vendor supply chains. We verify every cross-reference to ensure the replacement matches the E reinforced geometry and K tapered bore, not just the base digits. Batch traceability is maintained from the manufacturer’s production facilities directly to your receiving dock, providing complete transparency. Our technical team reviews the application parameters to confirm the selected variant aligns with your specific load and speed requirements. This rigorous validation process guarantees that the components you install are exactly what the equipment engineering demands.
To ensure the selected component perfectly matches your machinery, please provide the specific radial and axial load values, operating speeds, and expected thermal conditions. Sharing the original equipment manufacturer’s part number allows our engineering team to perform a rigorous cross-reference check against the required suffix configuration. We will evaluate your application parameters to confirm the internal clearance and mounting arrangement are optimized for your specific operating environment. This technical review guarantees you receive a fully validated solution ready for immediate installation.
Q: How does the K suffix affect the installation process compared to a cylindrical bore?
A: The 1:12 tapered bore requires mounting on a matching tapered shaft or using an adapter sleeve. This allows maintenance crews to precisely control the radial internal clearance by measuring the drive-up distance during installation. It ensures the bearing is locked securely in place while maintaining the exact operational clearance needed for thermal expansion in heavy-duty applications.
Q: What must be verified when cross-referencing the E suffix to other brands?
A: When cross-referencing, it is critical to confirm that the alternative brand’s equivalent also features the enhanced internal design with optimized roller profiles and cage guidance. Simply matching the base dimensions is insufficient, as a non-reinforced variant will lack the necessary dynamic load capacity and fatigue resistance required for high-vibration environments like vibrating screens and crushers.
Q: How can premature cage failure be prevented in high-vibration crushing equipment?
A: Preventing cage failure requires selecting the reinforced internal design and ensuring the correct internal clearance is achieved during mounting. Proper lubrication with high-viscosity grease capable of withstanding shock loads is essential. Additionally, verifying the shaft and housing tolerances prevents misalignment that would otherwise induce destructive edge stresses on the rolling elements and cage structure.
Q: What is the correct procedure for tightening the lock nut on an adapter sleeve?
A: The lock nut must be tightened to a specific angle or drive-up distance to achieve the target residual internal clearance. Over-tightening will excessively expand the inner ring, eliminating the clearance and causing thermal seizure during operation. Using a feeler gauge or dial indicator to measure the clearance reduction ensures the tapered interface is secured without compromising the bearing’s internal geometry.
Main shaft, gearbox, and generator bearings for onshore and offshore wind turbines. Engineered for 20+ year service life.
Crushers, conveyors, and processing equipment bearings designed to withstand shock loads and contaminated environments.
Rolling mill and continuous casting bearings rated for extreme temperatures, heavy loads, and aggressive lubricants.
Hub units, transmission, and electric motor bearings meeting TS 16949 requirements for passenger and commercial vehicles.
Machine tool spindle and robotics bearings with P4/P2 accuracy class for ultra-precise positioning and minimal vibration.
Pumps, fans, compressors, and conveyor systems across all manufacturing sectors requiring reliable, cost-effective bearing solutions.
Official partner since 1998 with direct access to SKF technical resources, genuine products, and engineering expertise.
In-house team provides application design, failure analysis, and predictive maintenance -- reducing bearing failures by 35%.
Every product undergoes rigorous pre-shipment inspection with full documentation for traceability and compliance.
Dedicated account managers and reliable delivery networks ensure on-time supply for enterprise clients worldwide.
Performance Metrics
35%
Failures Prevented
70%
Downtime Reduction
25+
Years Experience
24h
Quote Response
78% of large enterprises prefer suppliers offering integrated technical support and lifecycle services.
Custom bearing selection and system design based on your specific load conditions, speeds, temperatures, and environmental factors.
Root-cause investigation of bearing failures using metallurgical testing, vibration analysis, and operating data review.
IIoT-enabled monitoring with smart sensor bearings for real-time vibration, temperature, and RPM tracking.
Modified bearings with special coatings, seals, tolerances, or materials. Lead time 8-12 weeks from official channels.
Certified engineers available for on-site installation support, alignment checks, and commissioning assistance worldwide.
Long-term service agreements including regular maintenance checks, replacement scheduling, and performance reporting.
Free samples available for orders over $50K
Validated against your KPIs before full production commitment.
-- Get In Touch
Our certified engineers will review your application requirements and provide a detailed quote within 24 hours.
Address
No. 377 Bansongyuan Road, Huangpu District, Shanghai, China
Free Sample Program
Orders over $50K qualify for free product samples
Test against your KPIs before full production commitment. Ask our engineers for details.
Regarding: 21312EK Spherical Roller Bearing Tapered Bore Enhanced Load Capacity
-- Related Products

SKF Authorized Engineering Partner
Need technical support or a custom solution?
15+ certified engineers ready to help. Response within 24 hours.