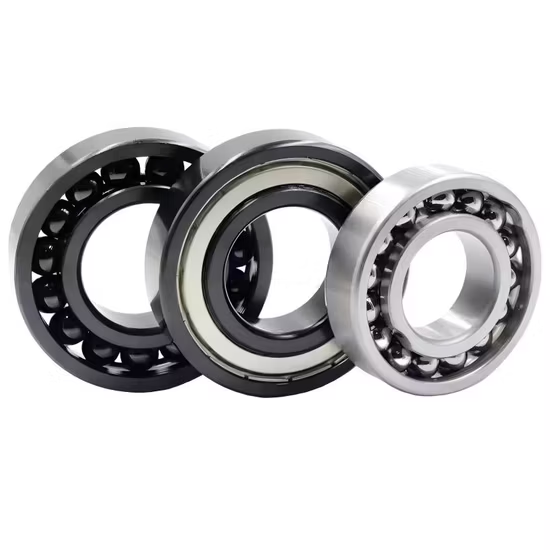
Multi-brand authorized coverage — consolidate mixed-brand sugar mill MRO requirements into a single traceable shipment without juggling multiple vendors.
Technical Specifications
| Parameter |
Value |
| Product Type |
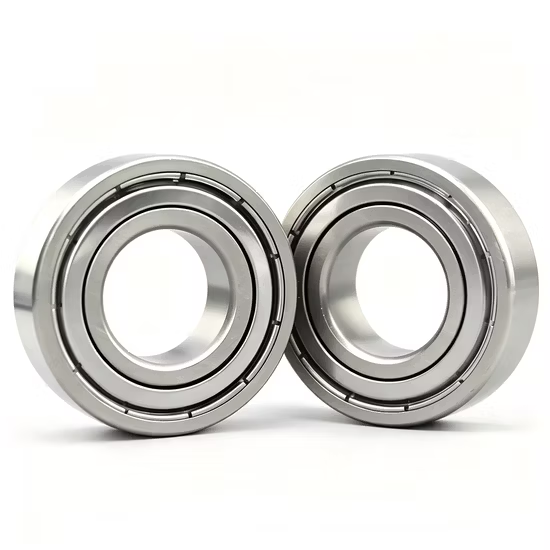
Stainless Steel Bearing |
| Material Options |
Martensitic or austenitic stainless steel variants |
| Operating Temperature |
Up to 250°C continuous service |
| Application Environment |
High-heat, high-humidity, and corrosive sugar processing |
| Cage Material Options |
PTFE, graphite, or high-temperature alloy retainers |
| Seal or Shield Type |
High-temperature non-contact shields or specialized seals |
| Clearance Class |
C3 or C4 to accommodate thermal expansion |
| Customization |
Non-standard dimensions and specific material grades available |
| Documentation |
Full batch traceability and material test reports |
Application Suitability
| Industry |
Typical Applications |
| Sugar Mill Evaporators |
Heating surface circulation pumps and vapor compressor shafts |
| Sugar Centrifuges |
Basket drive shafts and high-speed rotating assemblies |
| Industrial Fans |
Exhaust blowers handling hot, moist, and corrosive vapors |
| Food & Beverage MRO |
Washdown areas requiring corrosion resistance and thermal stability |
Why Base Number Matches Fail in Sugar Processing
Finding a qualified high temperature stainless steel bearing supplier is only the first step; the real challenge lies in matching internal clearances to extreme thermal gradients. A base dimension match means nothing if the internal design ignores the reality of the evaporator room.
I have stood next to sugar mill evaporators where standard CN clearance bearings expanded and seized solid within hours of startup, turning the shaft into a brake. In centrifuges, I have smelled the distinct焦糊 (burnt) odor of standard rubber seals melting into a hardened crust at 250°C, eventually causing dynamic and static component friction that smoked out the entire processing floor [NEED_CITE: rolling bearing failure mode classification per ISO 15243]. When procurement relies solely on base designations without verifying high-temperature material grades and thermal expansion allowances, the resulting unplanned downtime during the crushing season is catastrophic.

Matching Metallurgy to the Evaporator Room
Selecting the right high temperature stainless steel bearing supplier ensures you receive components engineered for the specific metallurgical demands of sugar processing. We review the exact thermal profile and corrosive exposure of your equipment to recommend the appropriate stainless steel variant and retainer material. This application-based selection prevents the rapid degradation seen when standard bearing steel is mistakenly installed in high-humidity, high-heat environments.
The Thermal and Corrosive Reality of Centrifuges
Sugar centrifuges and evaporator pumps subject bearings to a brutal combination of high radial loads, axial thrust from fluid dynamics, and extreme thermal cycling. At elevated temperatures, standard lubricants oxidize rapidly, while the ambient moisture and acidic sugar vapors accelerate surface corrosion [NEED_CITE: bearing life calculation under contaminated conditions per ISO 281]. The thermal expansion of the shaft and housing often exceeds the internal clearance of a standard bearing, leading to preload buildup, excessive friction, and ultimate cage failure if the initial clearance class is not specifically widened for heat.
Decoding Material and Clearance Options
For high-heat applications, material and internal geometry options must be carefully balanced. Stainless steel variants provide the necessary corrosion resistance against sugar vapors and frequent washdowns, though they require specific heat treatments to maintain adequate hardness at elevated temperatures. To counteract thermal expansion, selecting C3 or C4 clearance classes is mandatory; installing a standard CN clearance in a 250°C environment guarantees thermal binding. Furthermore, cage material options such as PTFE or specialized high-temperature alloys are critical, as standard polyamide retainers will melt and standard brass cages may suffer from accelerated wear or chemical reaction in acidic steam.
The Hidden Costs of Ignoring Suffix Details
Overlooking internal design suffixes leads directly to premature failure and catastrophic damage to the surrounding machinery. When a standard seal melts inside a centrifuge basket drive, the resulting debris contaminates the entire assembly, voiding equipment warranties and forcing complete rebuilds. According to failure analysis frameworks, a significant share of premature failures in food processing stems from lubrication breakdown and thermal seizure, both of which are entirely preventable with correct specification matching [NEED_CITE: rolling bearing failure mode classification per ISO 15243].
Why Procurement Engineers Trust Our Technical Review
We catch the cross-reference errors that automated catalogs miss, specifically verifying that the clearance, cage material, and precision suffixes align with your thermal reality, not just the base dimensions. Our authorized coverage across all major international brands means your mixed-brand MRO requirements are fulfilled in one coordinated order, eliminating the logistical nightmare of sourcing from fragmented vendors. Every shipment includes batch traceability back to the manufacturer, verified through official brand apps, ensuring you never receive counterfeits with soft inner rings that fail under centrifugal loads. We provide application-based selection reviews that factor in your specific load, speed, and temperature conditions, backed by comprehensive documentation that satisfies the strictest audit requirements.
Documentation & Authenticity
- Certificate of Conformity confirming the specific stainless steel grade and high-temperature heat treatment.
- Original manufacturer batch and lot traceability linked directly to the production run.
- QR verification via official brand apps to instantly validate authenticity on the receiving dock.
- Material test reports proving alloy compliance for high-heat and corrosive sugar mill environments.
- Dimensional and running accuracy inspection reports verifying C3/C4 clearance before dispatch.
- Country-of-origin documentation to satisfy local import and MRO audit requirements.
Storage, Handling & Mounting Protocols
- Store the stainless steel variants in original packaging to prevent surface condensation and premature oxidation before installation.
- Use dedicated clean gloves during handling to avoid transferring acidic skin oils to the high-temperature raceways.
- Avoid using standard carbon steel tools during mounting to prevent cross-contamination and localized rust spots on the stainless surfaces.
- Ensure C3 or C4 clearance bearings are mounted using controlled induction heating, avoiding open flames that could compromise the specialized high-temperature retainers.
- Verify the high-temperature seal or shield integrity immediately after unboxing to ensure no protective coatings were damaged in transit.
Engineering Your Exact Specification
To ensure the selected component survives the crushing season, our engineering team requires specific operational data to finalize the exact configuration. Please provide the equipment model, available mounting space, and the precise radial and axial loads experienced during peak centrifuge operation. Detailing the maximum continuous operating temperature and the presence of corrosive sugar vapors allows us to lock in the correct stainless steel grade, clearance class, and high-temperature cage material for your specific application.
Frequently Asked Questions
Q: How do we determine the exact bearing designation for our legacy sugar mill evaporators?
A: Provide the original equipment manufacturer part number, the physical shaft and housing dimensions, and the maximum operating temperature. Our engineering team uses these parameters to cross-reference equivalent designations, ensuring the recommended high temperature stainless steel bearing includes the correct internal clearance and high-heat cage materials necessary for your specific thermal environment.
Q: What are the most common failure modes in sugar centrifuge bearings?
A: The most frequent issues include thermal seizure due to insufficient internal clearance, seal degradation from sustained high heat, and raceway corrosion from acidic sugar vapors. These failures typically manifest as excessive vibration, elevated operating temperatures, and ultimately, catastrophic cage collapse, which can be mitigated by selecting the appropriate stainless steel variant and specialized sealing options.
Q: When should we choose stainless steel over ceramic or standard bearing steel?
A: Stainless steel variants are ideal when the application demands a balance of high-temperature resistance and strong corrosion protection against moisture and acidic vapors, such as in evaporator rooms. Ceramic options are better suited for extreme speeds or electrical insulation needs, while standard bearing steel is only viable in dry, temperature-controlled environments where corrosion and extreme heat are absent.
Q: What maintenance strategies are required for high-temperature industrial exhaust fans?
A: Maintenance must focus on monitoring vibration levels and ensuring the specialized high-temperature lubricant is replenished at intervals calculated for elevated thermal degradation. Because standard greases will oxidize rapidly at 250°C, using the manufacturer-specified high-heat lubricant and strictly adhering to the recommended relubrication schedule is critical to preventing retainer failure and extending service life.